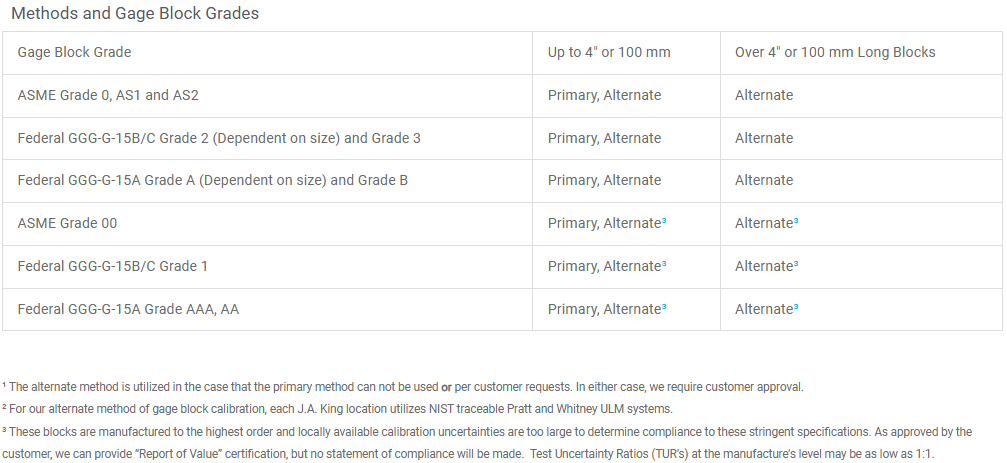
Below are methods used to calibrate gage blocks within all J.A. King network locations offering gage block calibration services.
Primary Method
Per national standards, the length of the gauge block is defined as the distance between a flat surface wrung to one end of the block, and a gauging point on the opposite end. The mechanical length of a gage block is the length determined by mechanical comparison of a block to another block of known interferometrically determined length. This mechanical comparison must be a measurement using two designated points, one on each end of the block taken at the witness point of the block.
For rectangular blocks, the witness point is in the middle of the block. For square blocks, the witness point is halfway between the hole and where the block is etched with the nominal size. Variation in Length (VIL) is also verified by mechanical comparison at each corner of the block.
Alternate Method¹
In some cases, gage block sets contain blocks that are not a standard size or we do not have a master block to compare it against. In these cases, we can offer an alternative method. This alternative method involves mastering on a block close to the nominal size and simply measuring the size of that blocks with a Universal Length Machine².
The uncertainties associated with this measurement shall be sufficiently small enough to determine compliance to the size specification provided by the manufacturer or customer. However, it is impossible to determine VIL (Variation in Length) as VIL requires the opposite side of the block to be rung against a base plate in a mechanical gage block comparator. Therefore a compliance statement to that grade cannot be made.
Methods and Gage Block Grades